
How tight tolerances affect precision aerospace alloy machining costs
For aerospace procurement teams, tight tolerances are more than a quality requirement. They directly influence quotation levels, supplier availability, delivery confidence, and the total cost of a qualified component.
In precision aerospace alloy machining, every additional micron of control can affect cutting parameters, tooling consumption, inspection methods, setup time, rework exposure, and production throughput.
The central buying question is not whether tighter tolerances cost more. They do. The practical question is whether each specified tolerance protects aircraft performance, safety, assembly function, or certification compliance.
Buyers who distinguish critical dimensions from merely conservative drawings can reduce sourcing cost without weakening engineering intent. That requires understanding how machining suppliers translate tolerances into operational risk.
Why Tolerance Bands Change Aerospace Machining Quotes
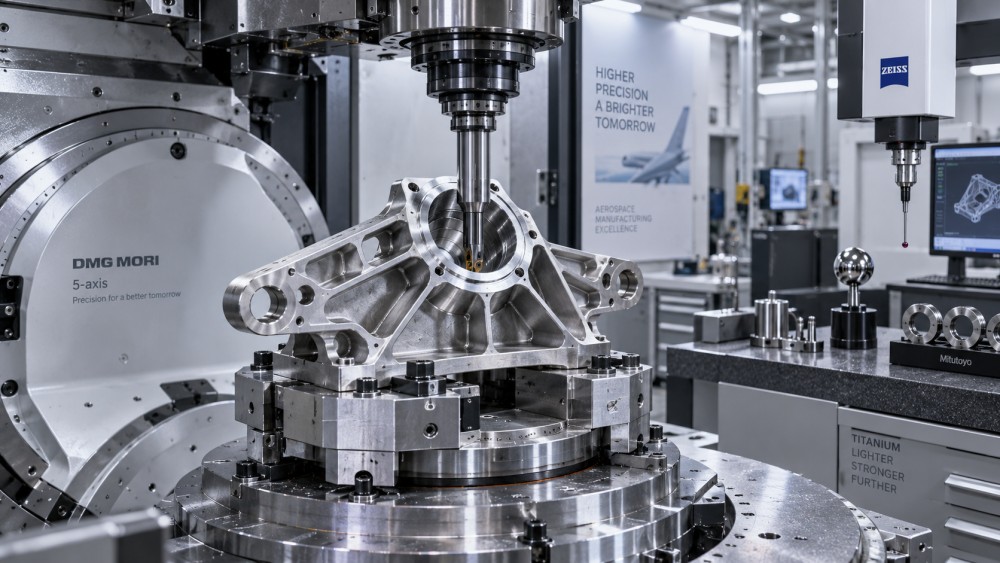
A tolerance is the acceptable variation around a nominal dimension. In aerospace parts, it may govern bore diameter, flatness, concentricity, profile, surface finish, wall thickness, or positional accuracy.
When the permitted range narrows, the supplier has less room to absorb normal variation from machine motion, tool wear, thermal expansion, material movement, and fixture deflection.
A dimension held at plus or minus 0.10 millimeters may be achievable through standard controlled machining. A requirement of plus or minus 0.01 millimeters often demands additional process engineering.
The price increase is rarely proportional to the number printed on the drawing. Reducing tolerance by half may require a different machine, slower finishing passes, specialized gauging, or complete inspection coverage.
Procurement teams should therefore avoid treating all dimensional callouts equally. A small group of tight features can drive the cost of an entire component because they control setup strategy.
For example, a thin-walled titanium bracket may contain mostly general tolerances, but one highly precise bearing bore can require dedicated fixturing and final machining after stress-relief operations.
The supplier must quote for the hardest feature, not the average feature. That is why two apparently similar aerospace parts can have materially different prices and lead times.
In precision aerospace alloy machining, tolerance requirements also influence whether a manufacturer can use proven existing capability or must develop a new validated production route.
Where the Cost Actually Appears
Machine time is the most visible cost driver. Tight tolerance features frequently require reduced feed rates, lighter finishing cuts, additional tool offsets, and repeat measurements between operations.
High-value aerospace alloys make this effect more pronounced. Titanium, Inconel, Waspaloy, and high-strength aluminum each respond differently to heat, cutting loads, springback, and residual stress.
Tooling costs rise when a shop must use premium end mills, reamers, boring bars, coated inserts, or custom form tools to achieve consistent feature geometry.
Tool life becomes less predictable as tolerances tighten. A tool can remain usable for roughing while becoming unsuitable for a final bore because its wear approaches the allowable variation.
Setup complexity is another major contributor. Close relationships between multiple features may require precision locating surfaces, repeatable clamps, probing routines, and carefully controlled workholding forces.
For flexible or thin-walled components, excessive clamping can distort the part during machining. Once released, the feature may move outside tolerance despite appearing correct on the machine.
Inspection requirements can add substantial cost. A standard caliper check differs greatly from coordinate measuring machine verification, air gauging, laser scanning, profilometry, or calibrated functional gauges.
When a customer requires 100 percent inspection, traceable inspection records, or first-article documentation, the supplier must allocate skilled quality resources and maintain a complete data trail.
Scrap risk also has a financial value. If a costly forged titanium blank fails its final tolerance check after several machining stages, the supplier may lose material, labor, tooling, and capacity.
Reliable suppliers include this risk in their pricing. An unusually low quote can indicate that a vendor has underestimated process variation, inspection effort, or nonconformance exposure.
Material Behavior Makes Tight Tolerances More Expensive
Aerospace alloys are selected for strength, fatigue performance, corrosion resistance, and elevated-temperature capability. Those same properties can make them difficult to cut accurately at commercial production rates.
Titanium alloys retain heat near the cutting zone, encouraging tool wear and thermal change. Nickel-based superalloys work-harden and impose high cutting forces on tools and fixtures.
Heat treatment condition matters as much as alloy designation. Material supplied in different tempers, forged states, or stress-relieved conditions can react differently during roughing and finishing.
Residual stress is particularly important in machined aerospace structures. Removing material from one side of a part can release internal stress and cause distortion after the component leaves the fixture.
A supplier may need staged roughing, stabilization time, heat treatment, or intermediate inspection before final finishing. Each added step improves predictability but adds handling, scheduling, and cost.
Thin walls, deep pockets, long slender features, and interrupted cuts amplify these issues. Tight tolerances on unstable geometries are generally more expensive than identical callouts on rigid prismatic parts.
Procurement professionals should ask suppliers which dimensions are process-sensitive, rather than assuming that all close tolerances have the same commercial impact across a drawing.
This discussion often reveals practical options, such as changing a datum sequence, allowing material at a nonfunctional surface, or separating precision finishing from earlier stock-removal operations.
How Tolerances Affect Lead Time and Supplier Capacity
Tight specifications can limit the pool of qualified suppliers. Many machine shops can process aerospace alloys, but fewer can repeatedly demonstrate precise capability with documented inspection and traceability.
Capacity is not simply the number of CNC machines available. It includes access to stable machines, experienced programmers, quality engineers, calibrated metrology equipment, and controlled environmental conditions.
A close-tolerance part may need to run on a high-accuracy five-axis machining center instead of an available general-purpose machine. This increases opportunity cost for the supplier.
Longer setup and inspection cycles reduce the number of parts completed per shift. When demand rises, these lower throughput rates can become more significant than direct machining labor.
First-article production is often the slowest phase. Suppliers may need process trials, fixture adjustments, offset studies, inspection feedback, and customer clarification before establishing repeatable production conditions.
For recurring programs, a validated process can reduce unit cost over time. However, buyers should not assume prototype pricing will automatically represent serial-production pricing or long-term capability.
Lead-time risk rises when the drawing leaves no recovery margin. If a critical feature fails near completion, the supplier may need replacement material, renewed machining slots, and repeated inspection.
For urgent aerospace maintenance or low-volume programs, paying for a more capable supplier may be economically preferable to accepting schedule uncertainty from a lower-priced quotation.
Which Tolerances Usually Deserve the Premium
Not every tight tolerance should be relaxed. Certain requirements are directly tied to safety, interchangeability, sealing, fatigue behavior, rotating balance, load transfer, and regulated airworthiness performance.
Bearing bores, mating interfaces, fuel-system sealing surfaces, fastener locations, turbine-related features, and precision actuator components often justify close dimensional control because their function depends on it.
Geometric tolerances deserve particular attention. Position, concentricity, flatness, perpendicularity, and profile controls may matter more than a simple linear dimension when parts must assemble repeatedly.
Surface finish can also be functional. It may influence sealing, coating adhesion, friction, crack initiation, fatigue resistance, or compatibility with a mating component.
The correct buying objective is not broad tolerance relaxation. It is targeted alignment between functional requirements, manufacturing capability, inspection plans, and the actual consequences of variation.
Ask engineering teams to identify critical-to-function and critical-to-quality features clearly. Those features should remain protected, while nonfunctional dimensions can use practical general tolerances where appropriate.
Functional stack-up analysis is especially useful for assemblies. It can reveal that one component has been over-specified because the actual assembly has sufficient clearance or adjustment elsewhere.
Where engineering authority permits, consider defining acceptance through functional gauges or interface requirements. This can be more useful than imposing unnecessarily restrictive dimensions on isolated features.
A Procurement Framework for Reviewing Expensive Quotes
When a quote for precision aerospace alloy machining appears high, start with the drawing rather than immediately requesting a discount. Ask the supplier to identify the top cost-driving features.
A capable manufacturer should explain whether the cost comes from tolerances, geometry, alloy machinability, inspection requirements, material yield, special processes, or low production volume.
Request a structured quotation that separates nonrecurring engineering, fixture development, first-article inspection, programming, material, machining, inspection, finishing, and recurring production costs where possible.
This structure helps buyers distinguish a genuine unit-cost problem from an upfront qualification investment. It also supports more meaningful comparisons between suppliers with different technical assumptions.
Review the tolerance scheme with the design authority before issuing a revised request for quotation. Changes should be based on function, interfaces, certification requirements, and documented engineering approval.
Ask whether selective tolerancing is possible. A supplier may hold a close requirement only after final finishing, while using broader controls during roughing and intermediate operations.
Clarify inspection expectations early. Requiring complete CMM reports for every part can be justified for certain programs, but it may be unnecessary for stable, proven, lower-risk characteristics.
For repeat orders, discuss statistical process control and sampling plans. Demonstrated process capability can reduce inspection burden while preserving confidence, provided customer quality requirements allow it.
Buyers should also verify the supplier's assumptions about datum structure, stock condition, heat treatment, coatings, masking, and post-machining operations. These details frequently affect final dimensional outcomes.
A quotation review should end with an agreed risk position. The lowest price is useful only when it is supported by a credible route to compliant parts, records, and delivery.
Questions to Ask Before Releasing a Purchase Order
Ask the supplier which dimensions create the greatest machining and inspection risk. Their answer should be specific to the drawing, alloy, batch size, and manufacturing sequence.
Ask whether the stated tolerances can be achieved consistently, not merely achieved once. Repeatability matters more than a one-off demonstration for aerospace production and replacement-part supply.
Confirm the planned inspection equipment and measurement uncertainty. Measuring a tolerance reliably requires an appropriate margin between the allowable variation and the gauge's actual capability.
Request evidence of similar work where confidentiality permits. Relevant experience includes comparable alloy families, geometry complexity, wall thickness, tolerance ranges, and aerospace documentation requirements.
Discuss material sourcing and traceability. Aerospace-grade bar, plate, forgings, and castings can have lead-time and certification implications that influence both cost and production risk.
Confirm whether downstream processes can change dimensions. Anodizing, plating, coating, heat treatment, shot peening, or welding may require machining allowances and carefully planned final inspection timing.
For critical parts, ask about contingency planning. A supplier should have a defined response for tool breakage, failed inspection, material nonconformance, machine downtime, and replacement stock.
Finally, ensure that commercial terms reflect technical reality. Unrealistic delivery commitments or penalty structures can encourage suppliers to conceal risk instead of escalating problems early.
Reducing Cost Without Diluting Aerospace Quality
The most effective savings usually happen before production begins. Early supplier involvement allows manufacturing specialists to identify tolerance conflicts before fixtures, programs, and material commitments are finalized.
Design-for-manufacturability reviews should focus on feature accessibility, tool reach, internal corners, wall stiffness, datum logic, tolerance stack-up, and opportunities to reduce secondary operations.
Standardizing recurring hole sizes, thread forms, radii, and inspection approaches can also improve sourcing efficiency. Small design choices can reduce custom tooling and setup variation across programs.
Combining parts is not automatically cheaper. A more complex monolithic component may eliminate assembly steps but demand expensive five-axis machining, costly material removal, and difficult close-tolerance control.
Likewise, splitting a component can introduce fastening, sealing, alignment, and qualification burdens. Procurement decisions should compare lifecycle economics instead of focusing only on piece-price estimates.
Long-term supplier relationships can create savings through process learning. Once fixtures, programs, inspection routines, and tool strategies are proven, repeat production often becomes more stable and efficient.
However, sustained savings require disciplined change control. Switching material sources, revising coatings, altering inspection frequency, or transferring suppliers can affect a previously capable process.
The strongest commercial outcome comes from matching required precision to verified function. That approach protects aerospace performance while directing premium manufacturing capability where it delivers real value.
Conclusion: Buy Precision Where It Protects Function
Tight tolerances increase precision aerospace alloy machining costs because they demand more controlled cutting, specialized tooling, stronger fixturing, deeper inspection, lower throughput, and greater scrap-risk management.
For procurement teams, the right response is not to challenge every premium or accept every drawing requirement without review. It is to connect each tolerance to functional necessity.
When buyers involve engineering and qualified suppliers early, they can identify cost-driving features, preserve mission-critical controls, reduce avoidable complexity, and make more defensible sourcing decisions.
In aerospace manufacturing, precision is valuable when it protects safety, fit, reliability, and compliance. Beyond that point, unnecessary precision becomes a recurring cost that informed procurement can prevent.