
Manufacturing execution systems justify their implementation cost when they convert fragmented shop-floor data into measurable improvements in quality, throughput, traceability, labor efficiency, and delivery performance.
For executives, the central question is not whether digital manufacturing matters. It is whether an MES can remove specific operating losses that currently consume margin, capacity, and customer confidence.
In welding automation, precision machining, power-tool assembly, and structural fastening, small process failures can create large financial consequences across rework, warranty exposure, delivery delays, and compliance risks.
A successful MES implementation does not begin with software selection. It begins by identifying where production decisions are delayed, records are unreliable, or process variation is expensive.
The strongest business cases usually involve constrained capacity, high-value components, complex routing, regulated traceability, frequent engineering changes, or persistent quality losses that existing systems cannot explain.
By contrast, a stable low-mix operation with simple routing, limited data requirements, and little manual reporting may not yet need a full manufacturing execution system.
Decision-makers should therefore evaluate MES as an operational investment, not a generic technology upgrade. The expected value must be linked to priority constraints and measurable performance indicators.
Start With the Cost of Operating Without Manufacturing Execution Systems
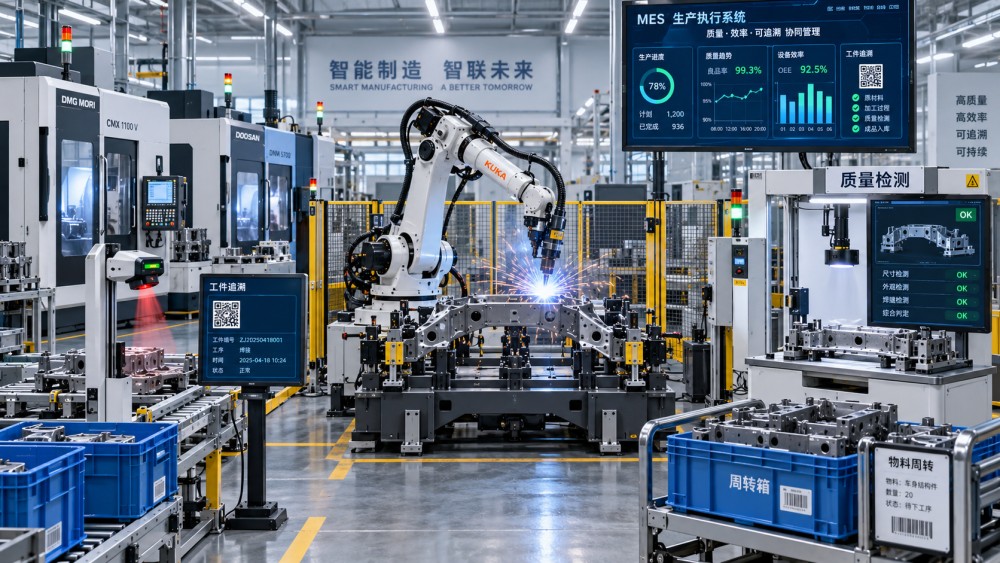
The implementation cost of manufacturing execution systems becomes easier to justify when leaders quantify the cost of current production blind spots rather than comparing only software licenses and integration fees.
Most factories already collect some information through ERP, spreadsheets, machine controls, paper travelers, quality logs, and supervisor experience. The problem is that these sources rarely provide one trusted operational record.
When data arrives late, managers cannot distinguish a temporary interruption from a recurring bottleneck. They may respond with overtime, expedited material, or additional equipment instead of correcting the real cause.
Consider a robotic arc welding cell producing structural frames. If weld defects are discovered only during final inspection, labor, consumables, fixtures, and downstream assembly time have already been consumed.
An MES can connect work orders, weld parameters, operator authorization, filler material batches, inspection outcomes, and repair codes. That connection makes the defect pattern visible while corrective action remains practical.
In CNC machining, the hidden cost often appears as unplanned tool changes, inconsistent offsets, idle machines awaiting instructions, or repeat scrap caused by obsolete programs and unclear revision control.
For fastener assembly, missing torque records or uncertain lot genealogy may not stop production immediately. However, those gaps can become extremely expensive during audits, field investigations, or customer containment actions.
The business case should include these losses in financial terms: scrap value, rework hours, delayed shipments, excess work in process, premium freight, warranty reserves, and supervisory time spent searching for answers.
Which Operating Conditions Create a Strong MES Business Case?
Manufacturing execution systems create the most value where production complexity exceeds the control capability of manual methods, disconnected applications, and informal communication between engineering, quality, logistics, and operations.
High product mix is a common trigger. As routings, work instructions, tooling, inspection plans, and approved parameters change across variants, paper-based control becomes vulnerable to execution errors.
Frequent engineering changes are equally important. When operators receive outdated drawings, weld programs, torque settings, or machining parameters, quality failures can occur before management recognizes the revision mismatch.
Traceability requirements strengthen the case further. Aerospace, rail, energy, medical, automotive, and heavy-equipment suppliers often need evidence linking each finished product to materials, processes, inspections, and personnel.
Capacity constraints also matter. A factory operating near its practical output limit may gain more from reducing waiting time and minor stoppages than from purchasing another welding robot or machining center.
Labor variability is another signal. If experienced supervisors are the only people who know which jobs are late, which fixtures are unavailable, or which machines need attention, operational risk is high.
MES is particularly useful when quality data exists but cannot be connected to production context. A defect count alone does not reveal whether failures correlate with a machine, shift, batch, program, tool, or material lot.
Finally, multi-site manufacturers benefit when local plants use different reporting habits. Standardized execution data can support comparable metrics without forcing every facility into identical production methods.
What Benefits Should Executives Expect, and What Should They Avoid Promising?
A credible MES case should focus on measurable operational outcomes rather than broad claims about digital transformation. The system must improve a metric that affects cost, revenue, risk, or capital efficiency.
Higher first-pass yield is often the clearest benefit. Guided instructions, parameter verification, automated checks, and defect feedback can prevent errors before defective work moves into expensive downstream stages.
Improved throughput is another common outcome, especially where work waits for material confirmation, program approval, quality release, maintenance response, or operator instructions that could be digitally coordinated.
Better schedule adherence can protect revenue without increasing physical capacity. Real-time work-order status helps planners identify at-risk operations early enough to adjust priorities, labor allocation, or subcontracting decisions.
Traceability can reduce containment costs after a quality event. Instead of quarantining broad inventory ranges, manufacturers can identify affected serial numbers, material lots, machines, and production windows precisely.
Labor productivity gains should be assessed carefully. MES rarely eliminates the need for skilled welders, machinists, quality personnel, or maintenance technicians, but it can reduce searching, recording, waiting, and repetitive reporting.
Inventory benefits can emerge through more accurate work-in-process visibility. However, leaders should not assume immediate reductions unless planning rules, material discipline, and transaction accuracy improve at the same time.
Executives should avoid promising that MES will automatically fix weak process engineering. Software can expose variation and enforce standards, but it cannot compensate for unstable fixtures, poor tooling, or unclear specifications.
How to Calculate Whether the Implementation Cost Is Financially Justified
The financial model should compare the fully loaded implementation investment with conservative, traceable benefits over a defined period, usually three to five years for enterprise manufacturing programs.
Investment should include software subscriptions or licenses, integration, master-data preparation, interfaces, hardware, network improvements, training, validation, process redesign, internal project time, and ongoing support.
Many business cases fail because internal effort is treated as free. Engineering, IT, quality, production, and maintenance personnel will spend substantial time defining workflows, testing transactions, and resolving data issues.
Benefits should be tied to baseline data. For example, calculate the annual cost of scrap and rework, then estimate only the portion that MES controls can realistically prevent.
For a welding operation, this may include reduced repair cycles, lower shielding-gas waste, fewer rejected assemblies, and less time spent reconstructing weld history after inspection failures.
For a machining facility, the model may include less idle time, fewer setup errors, improved tool-life monitoring, faster disposition of nonconforming parts, and reduced use of outdated CNC programs.
For torque-critical assembly, value may come from automated tool data capture, confirmation of fastening sequences, digital proof of completion, and faster response to customer traceability requests.
A practical hurdle is that annualized measurable benefits should exceed annual operating costs by a meaningful margin, while the initial investment should achieve an acceptable payback under conservative assumptions.
Scenario analysis is essential. Build a base case using achievable adoption levels, then test the impact of slower deployment, lower data quality, delayed integrations, and partial benefit realization.
Where Should a Manufacturing Execution System Be Deployed First?
Starting with the entire enterprise is rarely the best path. The first MES deployment should target a production area with visible pain, clear ownership, available data, and measurable economic consequences.
A constrained welding line is often a strong pilot candidate because the relationship between machine availability, weld quality, consumable usage, rework, and production output can be measured directly.
Complex machining cells also provide suitable starting points when they handle high-value parts, frequent program revisions, multiple inspections, expensive cutting tools, or demanding customer documentation requirements.
Another effective pilot is a torque-controlled assembly operation where missed fasteners, incorrect sequences, or incomplete records create safety, warranty, and compliance exposure beyond the immediate labor cost.
The first scope should include an end-to-end process, not merely a dashboard. It should connect work release, instructions, execution data, quality confirmation, exception handling, and operational reporting.
However, the pilot should not attempt every possible interface. Limiting initial integration to the systems needed for a usable workflow reduces technical risk and accelerates learning.
Success criteria must be agreed before deployment. Examples include lower rework hours, improved on-time completion, reduced manual transaction time, higher record completeness, or faster root-cause investigation.
A pilot that produces measurable improvement also creates a more reliable template for later rollout. It reveals training needs, data weaknesses, integration constraints, and governance decisions before enterprise scale increases complexity.
What Implementation Risks Can Erase the Expected Return?
The largest MES risk is treating implementation as an IT project rather than an operating-model change. Shop-floor adoption determines whether the new data reflects real production activity.
Over-customization is another frequent problem. Extensive bespoke functions can delay deployment, complicate upgrades, increase support costs, and preserve inefficient local practices that should have been reconsidered.
Poor master data can undermine even well-designed software. Incorrect routings, stale bills of materials, inconsistent machine names, and incomplete quality plans create confusion that users may blame on MES.
Weak executive sponsorship causes a different failure mode. Without clear authority, teams may avoid standardizing workflows, resolving ownership disputes, or requiring consistent transaction discipline across shifts and departments.
Training must address why each transaction matters, not only which button to select. Operators are more likely to record accurate information when they see how it prevents rework and protects product quality.
Integration complexity needs early scrutiny. ERP, quality management, maintenance, warehouse, machine connectivity, tool controllers, and labeling systems can each introduce timing, data ownership, and validation challenges.
Cybersecurity and system resilience also deserve attention, especially in connected plants. Access controls, network segmentation, backup procedures, and contingency workflows should be designed before production depends on digital execution records.
Finally, avoid measuring success only by go-live status. The real implementation milestone is sustained use that improves the chosen business metrics after initial stabilization has ended.
How Should Leaders Select the Right MES Scope and Vendor?
Vendor selection should follow process priorities. A polished demonstration has limited value unless the platform can support the actual routing, traceability, quality, integration, and usability requirements of the target operation.
Decision-makers should ask vendors to demonstrate realistic exceptions, including material substitutions, rework loops, engineering changes, failed inspections, machine downtime, and partial completion of complex assemblies.
For welding automation, evaluate how the solution captures parameters, links weld procedure specifications, records consumables, manages repairs, and integrates with robotic cells or seam-tracking equipment where required.
For precision machining, examine program control, setup verification, tool tracking, inspection integration, nonconformance workflows, and the ability to connect process data with part serial numbers.
For industrial fastening, assess support for connected tools, torque-angle results, sequence enforcement, error proofing, product genealogy, and retrieval of assembly evidence during customer or regulatory audits.
The vendor should also explain implementation responsibilities clearly. Manufacturers need to know which activities belong to internal operations, IT, systems integrators, machine suppliers, and the software provider.
Reference checks should focus on comparable complexity, not merely company size. A successful deployment in discrete, high-mix manufacturing is more relevant than a generic reference from another production environment.
Choose a platform that supports phased growth, but resist buying unused complexity. The right manufacturing execution system is the one that solves priority problems without burdening the organization with unnecessary configuration.
The Decision: When MES Is Worth the Investment
Manufacturing execution systems justify their implementation cost when a factory can identify operational losses that digital execution control can materially reduce, measure, and sustain after deployment.
The strongest candidates face a combination of quality risk, traceability pressure, constrained capacity, complex production routing, labor-dependent knowledge, frequent changes, or unreliable shop-floor visibility.
For leaders in welding, machining, tooling, and structural assembly, the investment should be evaluated through specific production economics rather than broad claims about smart manufacturing.
Start with the cost of defects, delays, missing records, manual reporting, and poor coordination. Then select a focused deployment area where better execution data can change daily decisions.
A disciplined pilot, conservative financial model, accountable process owners, and realistic integration scope will provide stronger evidence than an ambitious enterprise roadmap built on untested assumptions.
Ultimately, MES delivers value when it helps the organization produce the right part, with the right method, at the right time, while retaining reliable proof of how every critical step occurred.